
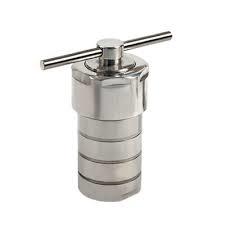
Understanding Autoclave Reactors: Key Insights for Industrial Applications
Autoclave reactors are specialized equipment used in various industrial processes to facilitate chemical reactions under controlled conditions of pressure and temperature. These reactors play a crucial role in sectors such as pharmaceuticals, petrochemicals, and materials science due to their ability to optimize reaction efficiency and product yield. One of the primary advantages of autoclave reac
08
2025
/
08
High Pressure Autoclave Reactors: A Game Changer for Chemical Engineering
High Pressure Autoclave Reactors: A Game Changer for Chemical Engineering Table of Contents 1. Introduction to High Pressure Autoclave Reactors 2. How High Pressure Autoclave Reactors Work 3. Applications of High Pressure Autoclave Reactors in Chemical Engineering 4. Advantages of Using High Pressure Autoclave Reactors 4.1 Enhanced Reaction Rates 4.2 Improved Yield and Selectivity 4.3 Versatility
07
2025
/
08

The Essential Guide to Centrifugal Canned Pumps: Understanding Their Applications and Benefits
Centrifugal canned pumps are specialized pumping devices designed to handle a variety of fluids across numerous industrial applications. These pumps are unique in their construction, featuring an integrated motor and pump casing that eliminates the need for traditional shaft seals. This design not only enhances reliability but also minimizes the risk of leakage, making centrifugal canned pumps an
06
2025
/
08

The Role of Wood Stove Heat Exchangers in Sustainable Heating
The Role of Wood Stove Heat Exchangers in Sustainable Heating Introduction to Wood Stove Heat Exchangers Wood stove heat exchangers play a pivotal role in enhancing the efficiency of wood-burning stoves while promoting sustainable heating solutions. As we increasingly seek alternative energy sources to combat climate change and reduce our carbon footprint, understanding the functionality and adv
05
2025
/
08

Exploring the Benefits of Stainless Steel Coil Tubing Heat Exchangers in Industrial Applications
Stainless steel coil tubing heat exchangers have gained significant attention in industrial applications due to their exceptional properties and effectiveness in transferring heat. These devices are designed to facilitate the efficient exchange of thermal energy between two or more fluids while maintaining the integrity and reliability of the system. Understanding the key benefits and applications
04
2025
/
08
GET A FREE QUOTE
If you are interested in our products and services, please contact us or leave us a message, we will serve you wholeheartedly
CONTACT : MR. GAO
Add : Yanbei Street, Qihe County, Dezhou City, Shandong Province


CONTACT : MR. JIAO
Add : Yanbei Street, Qihe County, Dezhou City, Shandong Province

Copyright : Shandong Raystone Chemical Material Co. , Ltd. Powerby : 300.cn jinan2 SEO BUSINESS LICENSE